Description
Product Overview
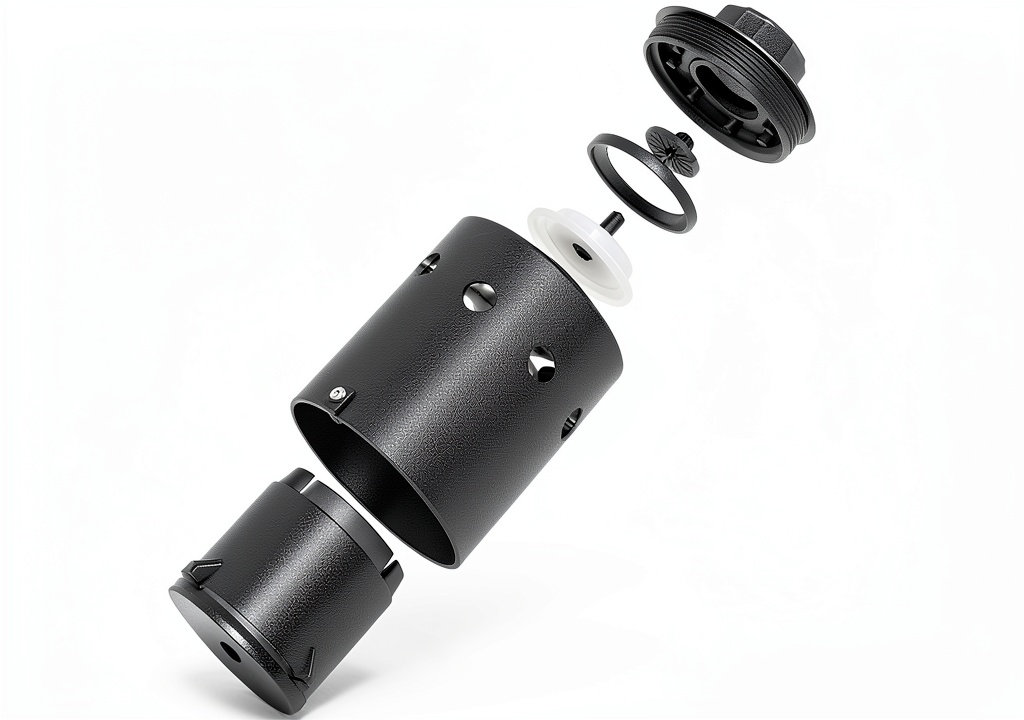
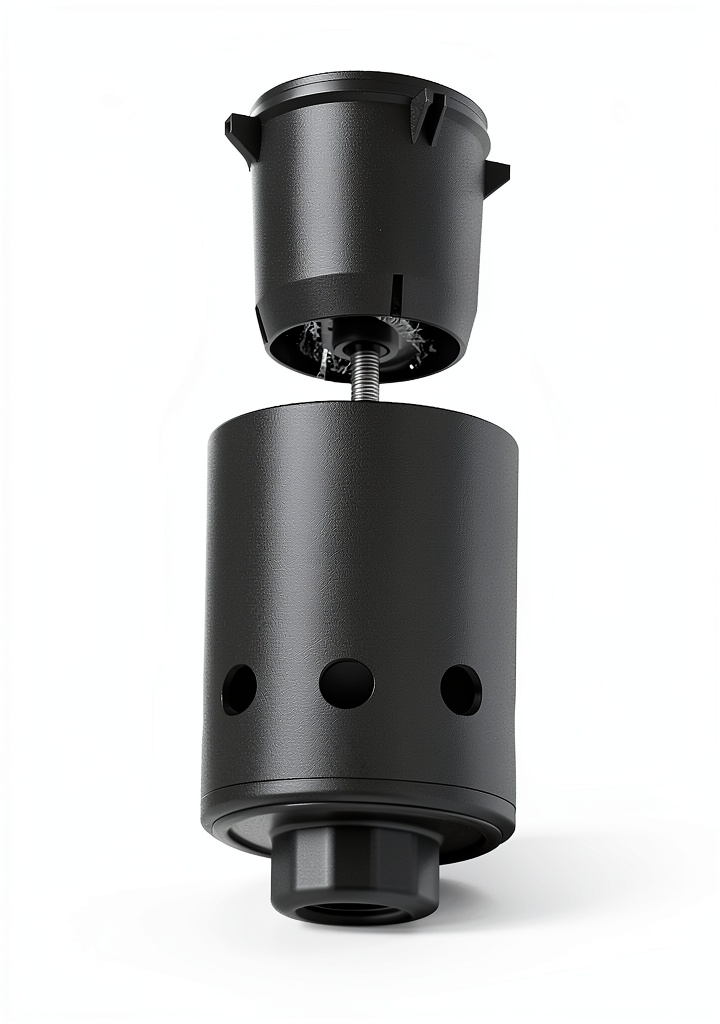
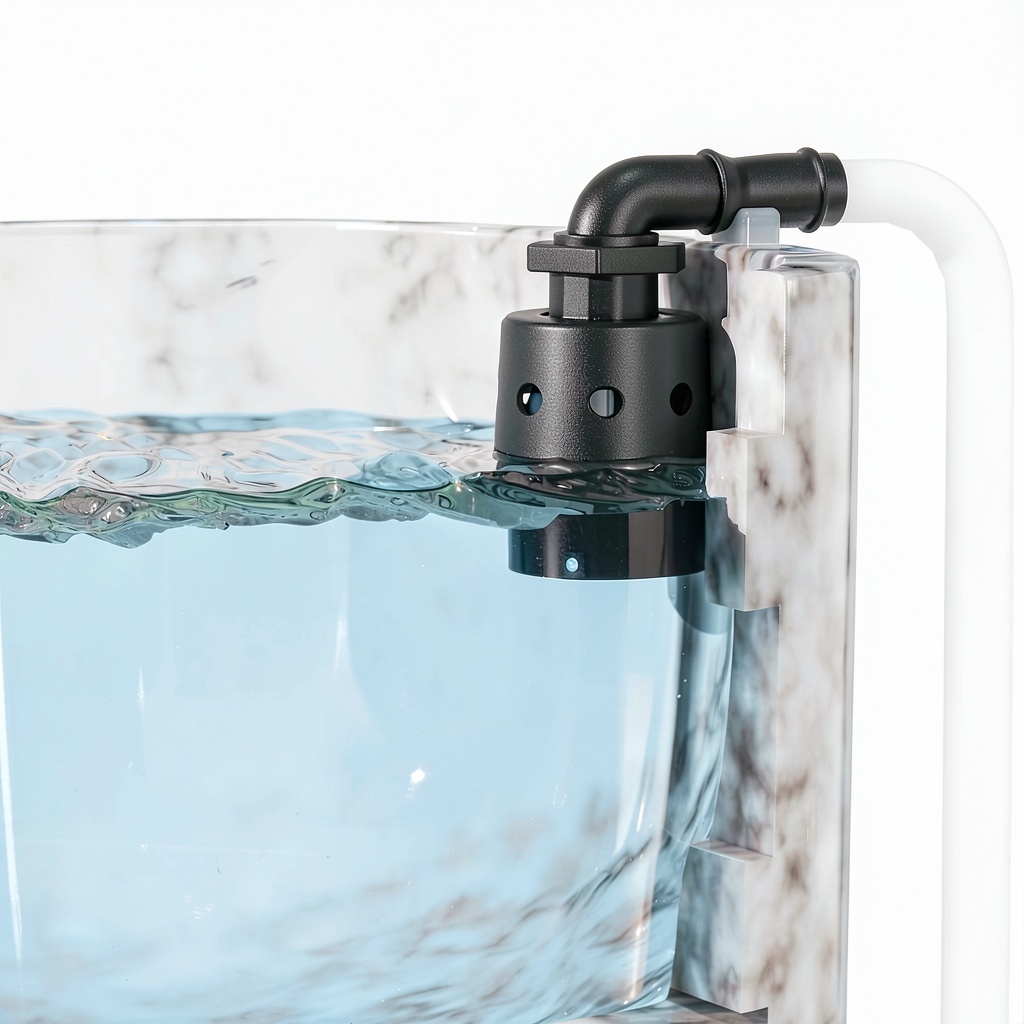
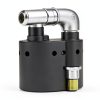
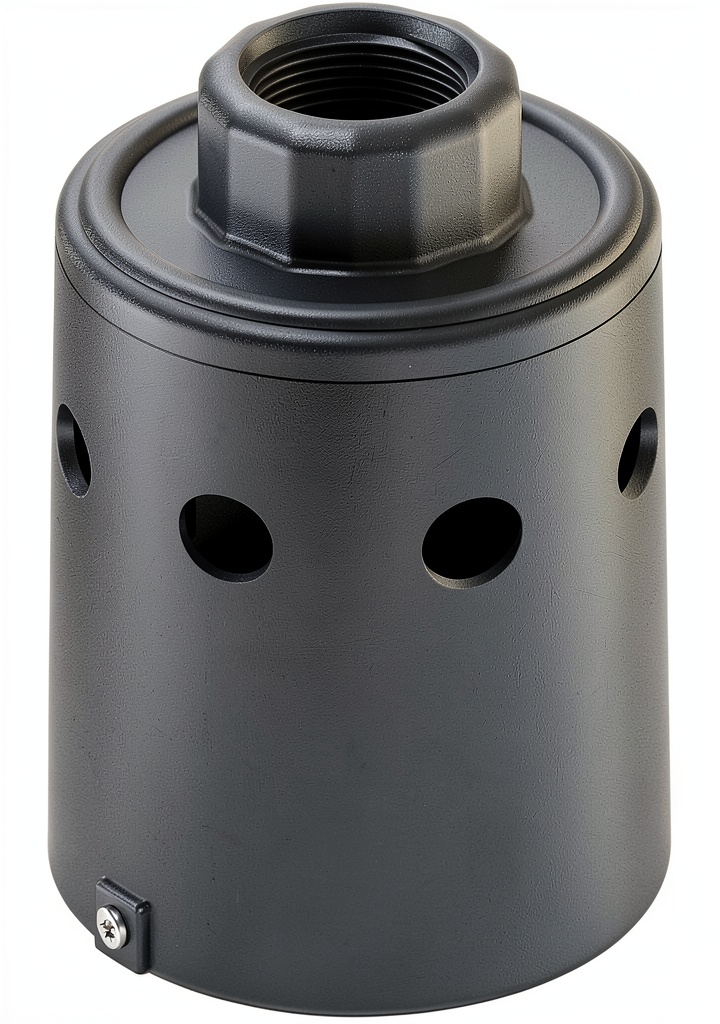
The Octina 1″ Float Valve is engineered from high‑grade nylon resin, a material chosen for its exceptional resistance to corrosion, ultraviolet radiation, and chemical exposure. Measuring 5 × 3.75 × 5 inches and weighing just 8.8 ounces, the valve offers a compact footprint that fits easily into a wide range of water storage containers. Its threaded 1‑inch inlet and NPS outlet connections provide a secure, leak‑free seal, while the valve’s internal mechanism is calibrated to operate reliably from 5 psi up to a maximum of 150 psi. The black‑finished exterior not only blends discreetly with most tank interiors but also adds an extra layer of protection against environmental wear. Every component, from the float arm to the sealing gasket, is molded as a single piece to eliminate weak points and ensure long‑term performance even under continuous cycling. The design also incorporates a low‑friction float that rises smoothly with water level changes, reducing wear and extending service life.
Installation of the Octina Float Valve is straightforward, requiring only basic plumbing tools and a standard 1‑inch threaded hose or mounting bracket. Applying plumber’s tape to the threads ensures a tight seal, and the valve can be mounted either vertically or horizontally depending on tank geometry. The valve’s single‑port configuration simplifies wiring and reduces potential leak points, while the NPS outlet allows direct connection to downstream piping or a discharge hose. Because the valve operates without electricity or batteries, it is ideal for remote locations where power is unavailable. The included user manual provides clear, step‑by‑step instructions, and the valve’s robust construction means it can withstand frequent opening and closing cycles without degradation. This makes it suitable for high‑traffic agricultural operations, commercial fish farms, and residential water storage solutions alike. Routine maintenance is limited to occasional visual inspection, making it a low‑maintenance solution for busy farm environments. Overall, the valve delivers reliable performance with minimal effort.
The valve’s technical specifications are designed to meet the rigorous demands of industrial and scientific applications. With a maximum operating pressure of 150 psi and a minimum functional pressure of 5 psi, it can handle sudden surges and low‑flow conditions alike. The 1‑inch inlet and outlet threads conform to standard NPT dimensions, facilitating easy integration with existing piping networks. At a weight of only 8.8 ounces, the valve adds minimal load to floating platforms or portable tanks. Its black nylon finish complies with ASTM D638 for polymer strength, ensuring that the component retains its structural integrity even after prolonged exposure to UV radiation and chemical agents commonly found in agricultural runoff. The valve also meets ISO 9001 quality management standards, reflecting Octina’s dedication to consistent manufacturing excellence and traceability throughout the production process. These certifications provide additional assurance for customers operating in regulated environments. Overall, the specifications ensure reliable operation across a broad spectrum of water handling tasks.
Compatibility with a broad range of fittings further enhances the Octina Float Valve’s versatility. The valve’s 1‑inch NPT threads are compatible with standard PVC, ABS, and metal pipe schedules, allowing seamless integration into existing water distribution networks. For users requiring a quick‑connect solution, adapters are readily available from Octina’s accessory line, enabling conversion to push‑fit or compression fittings without compromising seal integrity. The valve’s low profile design also permits installation in confined spaces such as under‑tank brackets or within compact pump housings, making it an ideal choice for retrofitting older systems that have limited clearance. This adaptability ensures that the valve can be employed across a spectrum of industrial, agricultural, and residential setups without the need for extensive re‑engineering. The valve also meets CE marking requirements for safety and environmental compliance, providing additional assurance for users operating within regulated markets. This compliance simplifies certification processes for commercial installations.
Usage
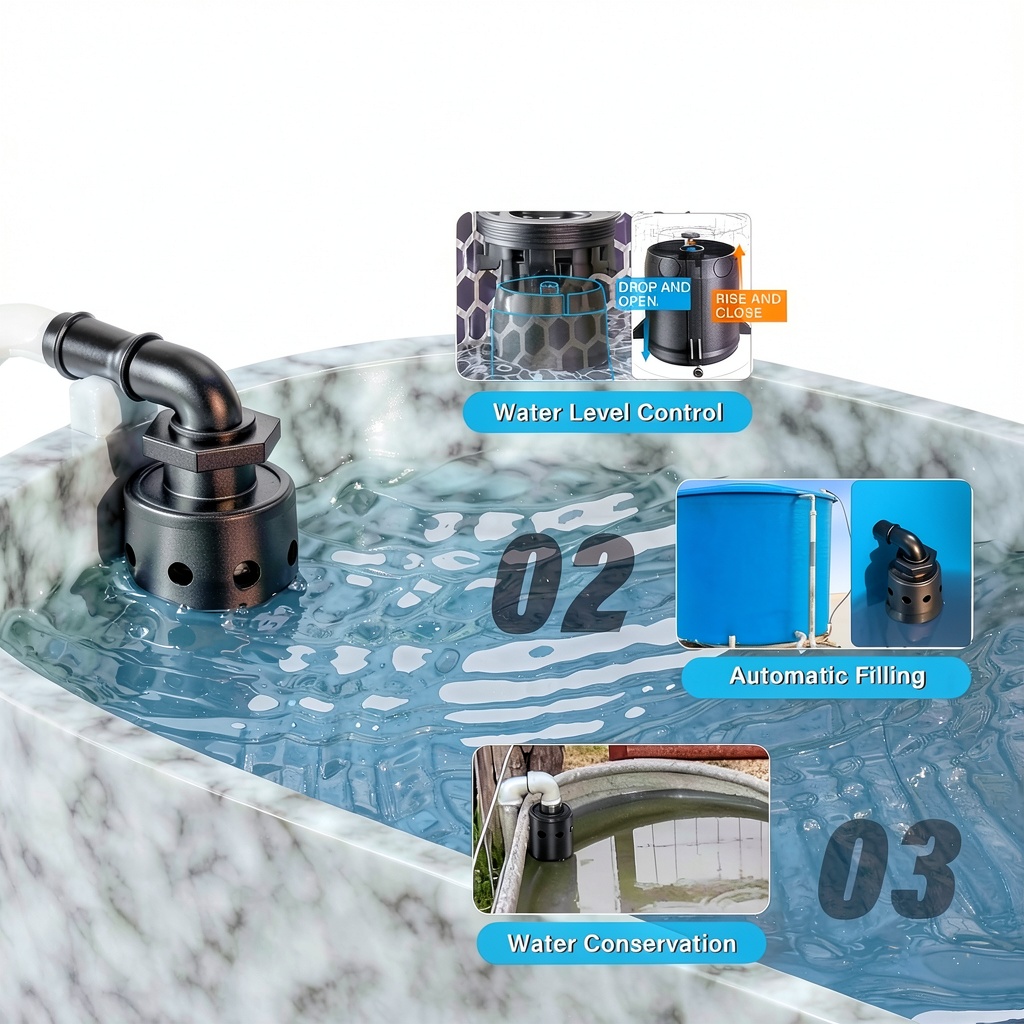
The Octina Float Valve excels in a variety of water management scenarios. In livestock troughs, it automatically refills the trough as animals drink, ensuring a constant supply of fresh water without the need for manual monitoring. For stock tanks used to store water for irrigation or emergency reserves, the valve maintains the desired water level, preventing both under‑filling and overflow during heavy rain events. Aquaculture facilities benefit from the valve’s precise control, allowing fish ponds to be kept at optimal depths for oxygen exchange and temperature regulation. The valve’s ability to operate across a wide pressure range also makes it suitable for rainwater harvesting systems, where fluctuating water levels can otherwise cause spillage or waste. By integrating the float valve into these applications, operators can reduce labor costs, improve water availability, and enhance overall system efficiency. Additionally, the valve’s silent operation ensures that it does not disturb animals or workers during routine farm activities.
Beyond simply filling tanks, the Octina Float Valve contributes to water conservation by preventing unnecessary overflow and runoff. When the water level reaches the preset float height, the valve automatically shuts off the inlet, eliminating wasteful discharge that can erode soil and carry contaminants into nearby waterways. This precise control is especially valuable in regions prone to drought, where every drop of stored water is critical for livestock health and crop irrigation. The valve’s nylon resin construction also means it does not leach harmful substances into the water, preserving water quality for both animal consumption and agricultural use. By maintaining optimal water levels, the valve helps extend the usable lifespan of stored water, reducing the frequency of refilling and the associated energy consumption of pumps. The automatic shut‑off feature also reduces the risk of flooding around the tank perimeter, protecting surrounding equipment and infrastructure. Overall, this leads to lower operational costs and a smaller environmental footprint for the entire water management system.
In addition to traditional livestock and aquaculture uses, the Octina Float Valve is well suited for residential rainwater harvesting barrels, garden irrigation reservoirs, and even small‑scale hydroponic systems. Homeowners can install the valve on a 55‑gallon rain barrel to automatically maintain a preset water level, preventing overflow during heavy storms and ensuring a ready supply for garden watering. For hydroponic growers, the valve can regulate nutrient solution levels in reservoirs, reducing the risk of pump cavitation and maintaining optimal plant health. The valve’s ability to function without electricity makes it an ideal component for off‑grid cabins and remote farms where solar or wind power may be the primary energy source. Moreover, the valve’s compact size allows it to be mounted on limited‑space containers, making it versatile for a variety of container dimensions and configurations. Its reliable operation reduces the need for manual monitoring, freeing up time for other farm or garden tasks.
Advanced users can integrate the Octina Float Valve into automated control systems using mechanical linkages or pressure‑sensing actuators. By coupling the valve’s motion to a relay, it can trigger alarms or send status updates to a central monitoring dashboard, enabling real‑time visibility of water levels across multiple tanks. This capability is especially valuable for large‑scale operations such as dairy farms or aquaculture facilities where dozens of water containers must be managed simultaneously. The valve’s silent operation ensures that the added automation does not introduce unwanted noise, preserving a calm environment for both livestock and workers. Moreover, the valve’s battery‑free design eliminates the need for power management, reducing maintenance complexity in remote monitoring setups. Integrating the valve with existing PLC systems is straightforward, as the mechanical output can be translated into digital signals using simple transducers, expanding its utility in modern smart‑farm infrastructures. This flexibility supports future scalability and system upgrades.
Why Choose Us
Octina has invested heavily in quality upgrades for this float valve, conducting hundreds of pressure and durability tests to verify performance from 5 psi up to the maximum 150 psi rating. The upgraded design features reinforced internal components that resist deformation under high pressure, while the external nylon resin body is molded to eliminate seams that could become leak points. This rigorous testing regime ensures that each valve leaving the factory meets strict industry standards for reliability and longevity. Customers benefit from a product that not only meets but exceeds typical expectations for float valves in demanding agricultural and aquaculture environments. The manufacturing process incorporates precision injection molding, which guarantees uniform wall thickness and consistent float buoyancy across every unit. Additionally, the valve undergoes a final visual inspection and functional test to confirm smooth operation before packaging. These quality controls translate into a longer service life, reducing the need for frequent replacements and minimizing downtime for water management systems.
Octina is a recognized name in industrial fittings and plumbing components, with a reputation built on decades of delivering reliable hardware to the agricultural, livestock, and water treatment sectors. The company’s commitment to customer satisfaction is reflected in its responsive technical support team, which is available to assist with installation queries, troubleshooting, and maintenance advice. Users can rely on a comprehensive warranty that covers manufacturing defects for a period of one year, providing peace of mind and confidence in the product’s durability. Octina also offers a network of authorized distributors and service centers, ensuring that replacement parts and expert assistance are readily accessible wherever the valve is deployed. The brand’s extensive experience also means that the float valve is designed to integrate seamlessly with a wide range of existing plumbing systems, reducing the need for additional adapters or custom fittings. This compatibility simplifies upgrades and ensures consistent performance across diverse installations. Overall, the brand’s compatibility simplifies upgrades and ensures consistent performance across diverse installations. This compatibility simplifies upgrades and ensures consistent performance across diverse installations. This compatibility simplifies upgrades and ensures consistent performance across diverse installations. This compatibility simplifies upgrades and ensures consistent performance across diverse installations. This compatibility simplifies upgrades and ensures consistent performance across diverse installations. This compatibility simplifies upgrades and ensures consistent performance across diverse installations.
Octina’s after‑sales service includes a dedicated hotline and email support that respond within 24 hours for most inquiries. The company provides detailed installation guides, video tutorials, and a searchable knowledge base to help users troubleshoot common issues without needing a technician. For customers who encounter a defective unit, Octina offers a hassle‑free return and replacement process, shipping a new valve at no additional cost. This level of support underscores the manufacturer’s confidence in the product’s design and its commitment to delivering value throughout the valve’s operational life. Octina periodically releases firmware‑free updates to the valve’s design, allowing existing customers to benefit from incremental improvements without having to purchase a completely new model. This proactive approach to product evolution helps maintain optimal performance and keeps the valve aligned with the latest industry standards. Customers can also subscribe to a newsletter for tips on water management best practices.
Octina’s commitment to sustainability is reflected in the choice of nylon resin, a material that can be recycled and has a lower environmental footprint compared to metal components that require extensive mining and processing. The manufacturing process utilizes energy‑efficient injection molding and minimizes waste by reusing excess polymer material. By extending the service life of the float valve through robust design and thorough testing, the product reduces the frequency of replacements, thereby decreasing overall material consumption. Customers who prioritize eco‑friendly solutions benefit from a valve that supports water conservation, reduces energy usage associated with pump operation, and aligns with green farming practices. In addition, Octina sources its raw materials from suppliers that adhere to responsible environmental policies, ensuring that the entire supply chain contributes to reduced carbon emissions and sustainable manufacturing practices. This holistic approach makes the float valve a smart choice for businesses aiming to meet corporate sustainability goals.
Field tests conducted on mixed‑use farms have shown that the Octina Float Valve maintains water levels within a 2‑centimeter tolerance over a six‑month period, even under fluctuating usage patterns and temperature extremes ranging from -10 °C to 45 °C. Farmers report a 30 % reduction in water waste and a noticeable decrease in pump cycling frequency, translating to lower energy bills and extended pump lifespan. One customer from Texas highlighted the valve’s ease of installation, noting that a single technician could set it up in under 15 minutes without specialized tools. Positive feedback also emphasizes the valve’s durability, with several users confirming that the nylon body shows no signs of cracking or discoloration after a full year of continuous operation. These real‑world results reinforce the manufacturer’s claims and provide confidence for new buyers seeking a proven solution for water level management. Overall satisfaction scores consistently exceed industry averages, making it a reliable investment for long‑term operations.
Octina’s global distribution network ensures that the Float Valve and its accessories are readily available in key markets across North America, Europe, and Asia. Regional distributors provide localized inventory, enabling fast shipping and reduced lead times for customers worldwide. In addition, Octina maintains regional service centers staffed with trained technicians who can assist with on‑site installation, calibration, and troubleshooting. This worldwide presence allows businesses to rely on consistent product availability and support, regardless of geographic location. The company also offers training webinars and technical documentation in multiple languages, further simplifying adoption for international users. Customers benefit from localized warranty registration, enabling quicker claim processing and ensuring that replacement parts are stocked within regional warehouses. Octina’s commitment to maintaining a robust supply chain minimizes downtime and supports continuous operation for critical water management systems. Such comprehensive coverage reinforces confidence for enterprises that depend on uninterrupted water flow for production and animal welfare.
Key Features
- Durable nylon resin body resists corrosion, UV exposure, and chemical damage for long‑term reliability.
- Automatic shut‑off at preset water level prevents overflow and conserves water without manual monitoring.
- Handles pressures from 5 psi to 150 psi, suitable for a wide range of tank sizes and applications.
- Easy installation with standard 1‑inch threaded inlet and NPS outlet, requiring only basic plumbing tools.
- Octina provides responsive technical support, a one‑year warranty, and hassle‑free replacement for defective units.
FAQ
How do I install the Octina Float Valve?
Start by turning off the water supply. Apply plumber’s tape to the 1‑inch threaded inlet and outlet connections. Attach the valve to the tank using the threaded inlet, then connect the outlet to your discharge hose or pipe. Tighten the connections securely, restore water flow, and adjust the float to the desired water level.
What pressure range can the valve operate within?
The valve is rated for a minimum operating pressure of 5 psi and a maximum of 150 psi, allowing it to function reliably in both low‑flow and high‑pressure environments.
Can the valve be used in outdoor environments?
Yes. The nylon resin construction is UV‑resistant and corrosion‑proof, making it suitable for outdoor installations such as rain barrels, livestock troughs, and fish ponds.
What maintenance is required for the float valve?
Periodic visual inspections are recommended to ensure the float moves freely and the connections remain tight. No routine cleaning is needed unless debris accumulates in the inlet; in that case, briefly flush the inlet with clean water.
Reviews
There are no reviews yet.